Engineering Overview: Two-Ferrule Compression Technology
Shrushti Metal is a premier ISO 9001:2015 certified manufacturer, stockist, and global exporter of high-integrity Double Ferrule Tube Fittings located at the epicentre of India's metal trading hub in Kumbharwada, Mumbai. Engineered specifically for critical instrumentation, process control loops, high-pressure hydraulic lines, and hazardous fluid transfer, our two-ferrule compression fittings provide a reliable, gas-tight, metal-to-metal seal capable of withstanding extreme pressure spikes, cyclic thermal variations, vacuum conditions, and mechanical vibration.
Unlike traditional single-ferrule fittings or welded joints, the double-ferrule mechanical compression design separates the two vital engineering functions of a tube fitting: pressure containment / sealing and tube gripping / mechanical retention. This separation ensures that no rotational torque is transmitted from the fitting nut to the tubing during installation, preserving the metallurgical integrity of thin-walled and thick-walled tubing alike.
Anatomy of the 4-Piece Fitting Assembly
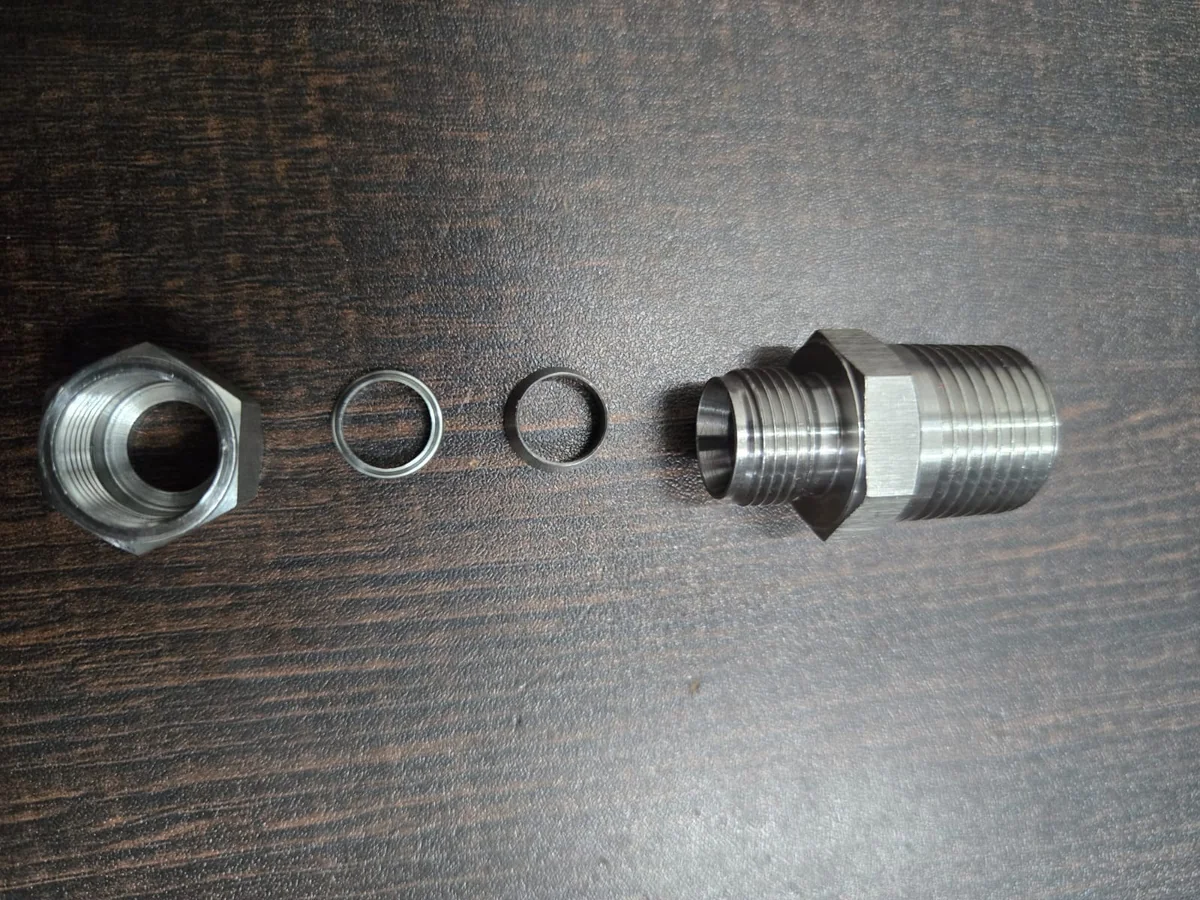
Figure 1: Exploded View of Shrushti Metal Double Ferrule Compression Assembly — Compression Nut, Back Ferrule, Front Ferrule, and Fitting Body.
1. Fitting Body
Precision CNC-machined from cold-drawn bar stock or heavy forgings. Features a micro-finished 10–16 RMS internal sealing taper and robust hex flats for wrench hold.
2. Front Ferrule
Acts as the primary fluid and gas barrier. During tighten-up, it is driven forward into the body taper and driven downward to compress circumferentially onto the tube OD.
3. Back Ferrule
Specially engineered with case-hardened rear geometry to bite into the tubing wall, creating deep axial retention, dampening system vibration, and preventing tube blow-out.
4. Compression Nut
Silver-plated interior threads eliminate friction and cold-welding. Transfers axial thrust smoothly into the back ferrule with minimal torque required by the pipefitter.
Technical Specifications & Standards Matrix
Every Shrushti Metal double ferrule fitting is manufactured to strict global engineering standards, guaranteeing dimensional interchangeability with international instrumentation standards.
| Fitting Type | Two-Ferrule Mechanical Compression Instrumentation Fittings |
|---|---|
| Components | 4-Piece Assembly: Body, Front Ferrule, Back Ferrule, and Silver-Plated Nut |
| Fractional Tube Sizes | 1/16", 1/8", 3/16", 1/4", 5/16", 3/8", 1/2", 5/8", 3/4", 7/8", 1", 1-1/4", 1-1/2", 2" OD |
| Metric Tube Sizes | 2mm, 3mm, 4mm, 6mm, 8mm, 10mm, 12mm, 14mm, 15mm, 16mm, 18mm, 20mm, 22mm, 25mm, 28mm, 32mm, 38mm, 50mm OD |
| Thread Specifications | NPT (ASME B1.20.1), BSPT / PT (ISO 7/1), BSPP (ISO 228/1), Metric ISO 261, SAE/MS straight threads |
| Working Pressure Rating | Vacuum up to 10,000 PSI (689 bar) — matched to maximum allowable working pressure of compatible tubing |
| Operating Temperature | -196°C to +649°C (-321°F to +1200°F) depending on material grade and seal selection |
| Sealing Method | Elastic / plastic metal-to-metal burnishing seal; zero elastomers, O-rings, or chemical sealants required |
| Brand Interchangeability | 100% intermixable and interchangeable with Swagelok, Parker A-LOK, Dk-Lok, Gyrolok, Sandvik |
| Quality Standards | ISO 9001:2015, CE Marking, ASTM A276, ASTM A182, ASTM A403, ASTM A234, EN 10204 Type 3.1 |
Material Grades & Metallurgy
The selection of raw material grade directly dictates corrosion resistance, fatigue limit, and pressure containment in severe operating environments. Shrushti Metal stocks and custom-manufactures double ferrule fittings in premium certified Stainless Steel and Alloy Steel grades:
1. Stainless Steel Alloys (ASTM A403 / ASTM A182 / ASTM A276)
Stainless steel is the standard choice for general industrial, marine, chemical, and analyzer sampling installations due to its superior chromium-nickel passivation layer:
| Material Grade | International Standard | Key Characteristics | Typical Applications |
|---|---|---|---|
| SS 316 / SS 316L | ASTM A403 / A182 WP316 / WP316L, 00Cr17Ni14Mo2 | 2-3% Molybdenum addition for pitting resistance against chlorides; low carbon prevents carbide precipitation. | Offshore oil & gas platforms, chemical refineries, marine instrumentation lines. |
| SS 304 / SS 304L | ASTM A403 / A182 WP304 / WP304L, 00Cr19Ni10 | Classic 18/8 austenitic stainless steel with excellent ductility, weldability, and economical general corrosion resistance. | Pneumatic logic controls, food & beverage processing, nitrogen and water lines. |
| SS 321 / 321H | ASTM A403 / A182 WP321, 1Cr18Ni9Ti | Titanium-stabilized stainless steel resisting chromium carbide formation up to 870°C (1600°F). | Thermal boiler feed loops, exhaust manifolds, petrochemical furnace analyzer tubes. |
2. High-Strength Alloy Steels (ASTM A234 / ASTM A182)
For extreme high-temperature steam distribution, power generation boilers, and hydrocracking units where creep-rupture strength is critical:
| Material Grade | Standard Designation | Alloy Composition | Operating Characteristics |
|---|---|---|---|
| Alloy Steel WP11 / P11 | ASTM A234 WP11, 15CrMo | 1.25% Cr - 0.5% Mo | High creep strength at temperatures up to 550°C in high-pressure steam headers. |
| Alloy Steel WP22 / P22 | ASTM A234 WP22, 12Cr2Mo1 | 2.25% Cr - 1.0% Mo | Superior resistance to hydrogen embrittlement and thermal fatigue in cracking furnaces. |
| Alloy Steel WP91 / P91 | ASTM A234 WP91, 10CrMo910 | 9% Cr - 1% Mo - V - Nb | Advanced martensitic alloy for supercritical and ultra-supercritical power boilers up to 600°C. |
| Special Cr-Mo Alloys | ASTM A234 WP5, WP9, 16MnR, 12Cr1MoV, Cr5Mo | Chromium-Molybdenum-Vanadium | Tailored for heavy industrial petrochemical reforming and high-velocity slurry piping. |
Fitting Types & Geometries in Stock
Shrushti Metal supplies every required geometric configuration to complete complex instrumentation runs without unnecessary adapters or pipe joints:
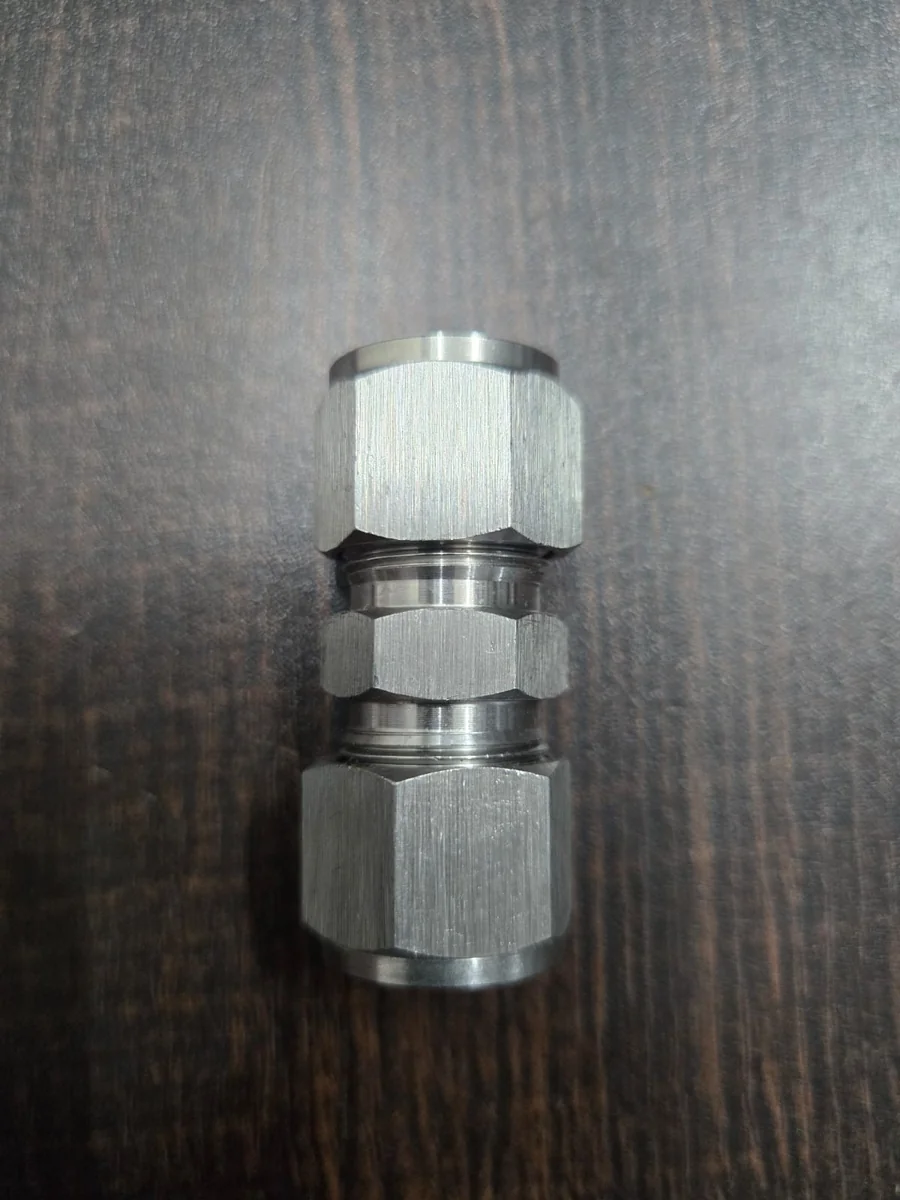
Straight Union
Connects two tubes of identical fractional or metric OD in a straight run with zero leakage.
Reducing Union
Smoothly transitions between two different tube sizes (e.g., 1/2" to 1/4" OD or 12mm to 6mm OD).
Bulkhead Union
Enables leak-tight tubing passage through control panels, firewall bulkheads, and analyzer enclosures.
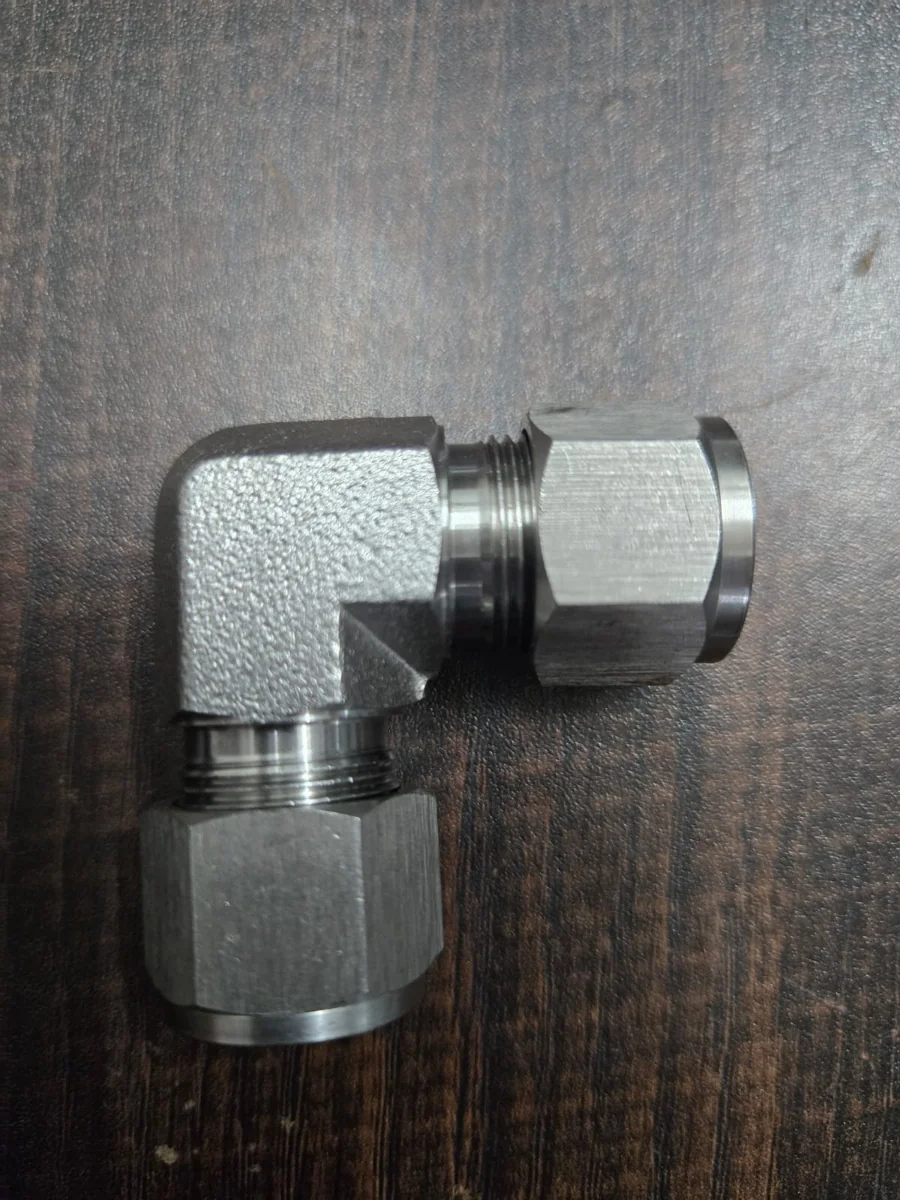
Union Elbow (90° & 45°)
Allows precise directional routing around equipment obstacles without inducing tube bend stresses.
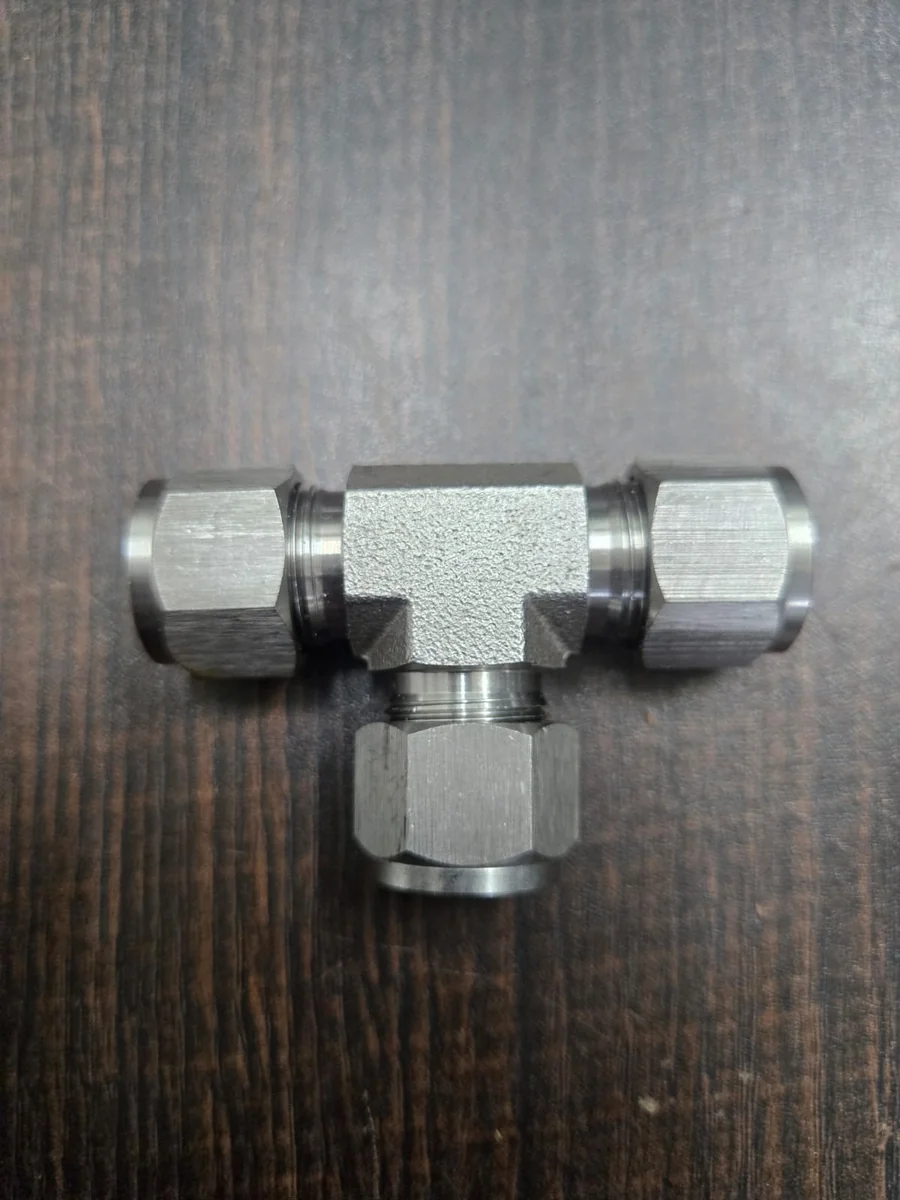
Union Tee & Reducing Tee
Splits flow into branch lines with balanced hydraulic flow and consistent wall-thickness containment.
Union Cross
Four-way junction designed for sensor manifolds, sampling trees, and multiport distribution headers.
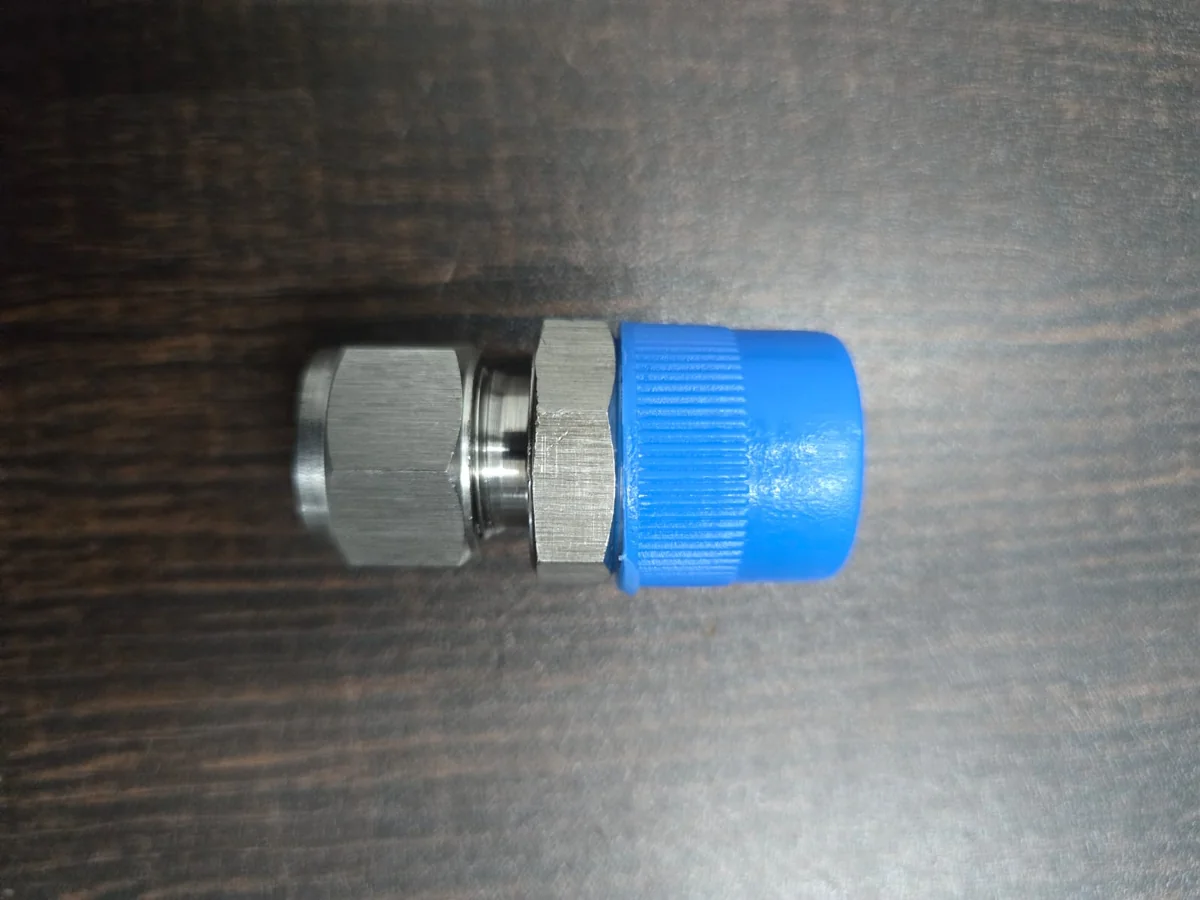
Male / Female Connector
Connects tubing directly to NPT, BSPT, or BSPP pipe threads on valves, manifolds, pumps, and regulators.
Caps & Plugs
Provides complete system isolation for unused ports or temporary pressure testing lines.
Working Pressure Ratings (PSI) by Tubing OD & Wall Thickness
A double ferrule fitting is engineered to possess a higher pressure holding capacity than the tubing it grips. The table below outlines the maximum allowable working pressures for fully annealed seamless 316 Stainless Steel tubing assembled with Shrushti Metal double ferrule fittings at ambient temperatures (-28°C to 38°C):
| Tube OD (Inches) | 0.028" Wall | 0.035" Wall | 0.049" Wall | 0.065" Wall | 0.083" Wall | 0.095" Wall | 0.109" Wall |
|---|---|---|---|---|---|---|---|
| 1/8" (0.125") | 8,500 PSI | 10,900 PSI | — | — | — | — | — |
| 1/4" (0.250") | 4,000 PSI | 5,100 PSI | 7,500 PSI | 10,200 PSI | — | — | — |
| 3/8" (0.375") | — | 3,300 PSI | 4,800 PSI | 6,500 PSI | — | — | — |
| 1/2" (0.500") | — | 2,600 PSI | 3,700 PSI | 5,100 PSI | 6,700 PSI | — | — |
| 3/4" (0.750") | — | — | 2,400 PSI | 3,300 PSI | 4,200 PSI | 4,900 PSI | 5,800 PSI |
| 1" (1.000") | — | — | — | 2,400 PSI | 3,100 PSI | 3,600 PSI | 4,200 PSI |
* Ratings calculated in accordance with ASME B31.3 Process Piping Code at allowable stress S = 20,000 PSI. For gas service, ensure tube wall thickness is adequate to prevent tube collapse under ferrule swaging.
Step-by-Step Installation & Gap Inspection Guide
Correct installation guarantees 100% leak-proof reliability across thousands of operating hours. Follow these standard engineering instructions for initial pull-up and remake:
-
1
Square Cut & De-burr the Tubing
Cut the stainless or alloy tubing squarely using a high-precision tube cutter or fine-tooth hacksaw. Gently de-burr the inside and outside edges of the tube end to prevent gouging the internal fitting seal seat.
-
2
Bottom the Tube in the Fitting Body
Insert the tube fully into the Shrushti Metal fitting body until it firmly bottoms out against the internal shoulder. Hand-tighten the compression nut until finger-tight.
-
3
Mark the Nut & Body Alignment
Scribe a visible reference mark at the 6 o'clock position across both the nut and fitting body flats using an inspection marker or scribe tool.
-
4
Perform the 1-1/4 Turn Pull-up
While holding the fitting body stationary with a backup wrench, rotate the nut 1-1/4 turns (1 turn and 90 degrees) to the 9 o'clock position. (Note: For smaller sizes 1/16", 1/8", and 3/16", rotate only 3/4 turn).
-
5
Verify with Gap Inspection Gauge
Position a standard gap inspection gauge between the nut and body hex flats. If the gauge cannot enter the gap, the fitting is properly tightened. If the gauge enters, further tightening is required.
100% Interchangeability & Intermixability Guarantee
A major concern for plant instrumentation managers and procurement engineers is legacy equipment compatibility. Shrushti Metal double ferrule fittings are engineered with precision computer numerical control (CNC) machining that adheres to universal instrumentation tapers, thread angles, and ferrule geometries.
This interchangeability allows engineering procurement teams to immediately reduce MRO replacement costs by 30% to 50% compared to multinational OEM list prices while securing same-day dispatch from our Mumbai central warehouse.
Quality Assurance, Testing & Third-Party Inspection
At Shrushti Metal, quality assurance is an unbroken chain starting from raw steel ingot chemistry verification to final pneumatic bubble leak testing:
- 100% Raw Material PMI: Positive Material Identification (XRF Analyzer) ensures exact elemental composition of Chromium, Nickel, and Molybdenum before machining commences.
- Hydrostatic Proof Testing: Every production batch undergoes hydrostatic pressure testing up to 1.5 times the rated working pressure in compliance with ASME standards.
- Helium Mass Spectrometer Testing: Detects micro-leak rates below 1 x 10⁻⁹ std cm³/s for ultra-pure gas and vacuum applications.
- Nitrogen Pneumatic Leak Testing: Conducted submerged in de-mineralized water to verify zero bubble formation at 1,000 PSI air pressure.
- Mill Test Reports: Issued with full chemical, physical, and heat-treatment traceability in accordance with EN 10204 Type 3.1.
- 3rd-Party Agency Clearances: Regularly inspected and approved by Lloyd's Register, TUV India, Bureau Veritas, DNV, TATA Projects, and L&T.
Major Cities We Supply To (South India & Pan-India)
Shrushti Metal supplies ex-stock materials daily from our Mumbai central steel hub in Kumbharwada to key industrial corridors across Southern India. With established logistics tie-ups with leading freight carriers (V-Trans, TCI Express, SafeXpress), shipments reach southern hubs within 24 to 48 hours: